Winder roller reconditioning — Reifenhäuser
Chrome plating and polishing of the working surface
We turned the damaged roller surface down to a diameter below the depth of the damage. We then carried out grinding, chrome plating, regrinding and polishing. After completing the work, we measured the surface roughness.
Send photos of the damage and the basic roller dimensions.
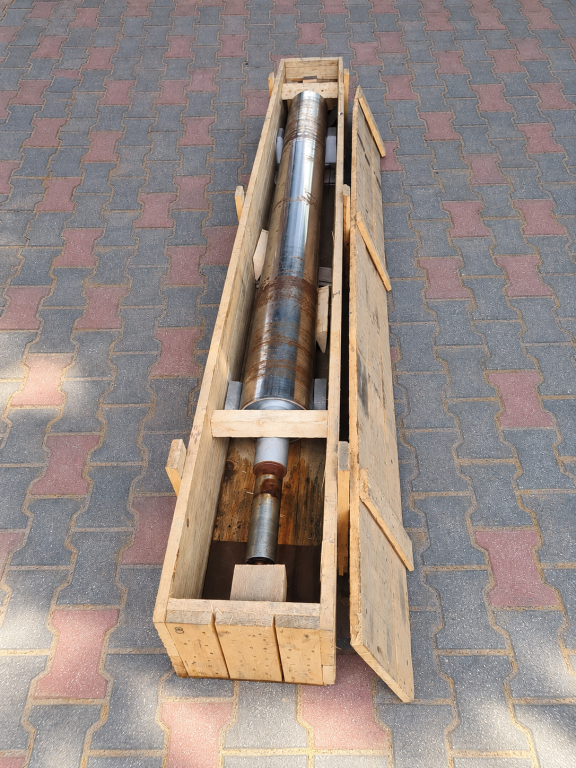
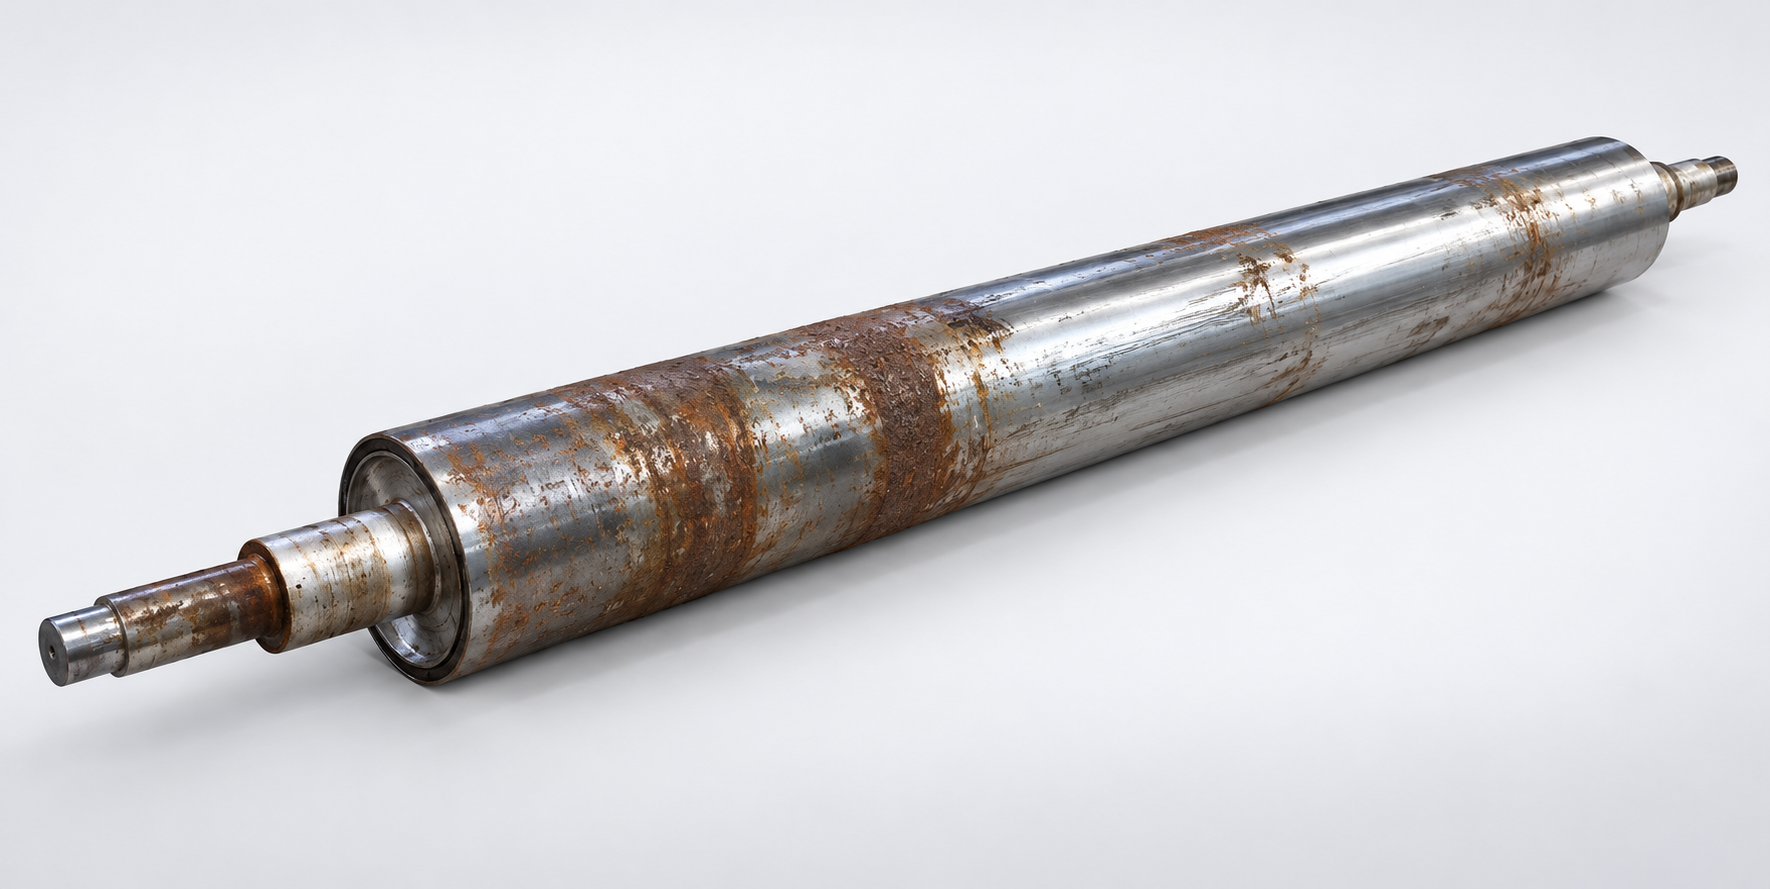
COMPONENT CONDITION BEFORE REPAIR
Scope of winder roller reconditioning
The repair covered the damaged working surface of the roller. Its condition required removing material down to a diameter below the depth of the damage, followed by surface preparation for chrome plating and finishing.
The scope of work was determined by the condition of this particular component. The journals and bearing seats were in good condition and did not require repair.
FIVE MACHINING AND FINISHING STAGES
Turning, grinding and chrome plating
We reconditioned the roller in five consecutive stages, from removing the damaged layer of material to polishing and surface roughness measurement.
- 01
Turning
We removed material down to a diameter below the depth of the surface damage.
- 02
Grinding before chrome plating
We ground the roller surface before applying the coating.
- 03
Chrome plating
We applied a chrome coating to the prepared roller surface.
- 04
Grinding after chrome plating
We machined the applied coating.
- 05
Polishing
We finished the surface and then measured its roughness.
BEFORE AND AFTER RECONDITIONING
From a damaged surface to a finished coating
Surface requiring reconditioning
The surface damage required turning the roller down to a diameter below the depth of the damage and preparing it for further machining.
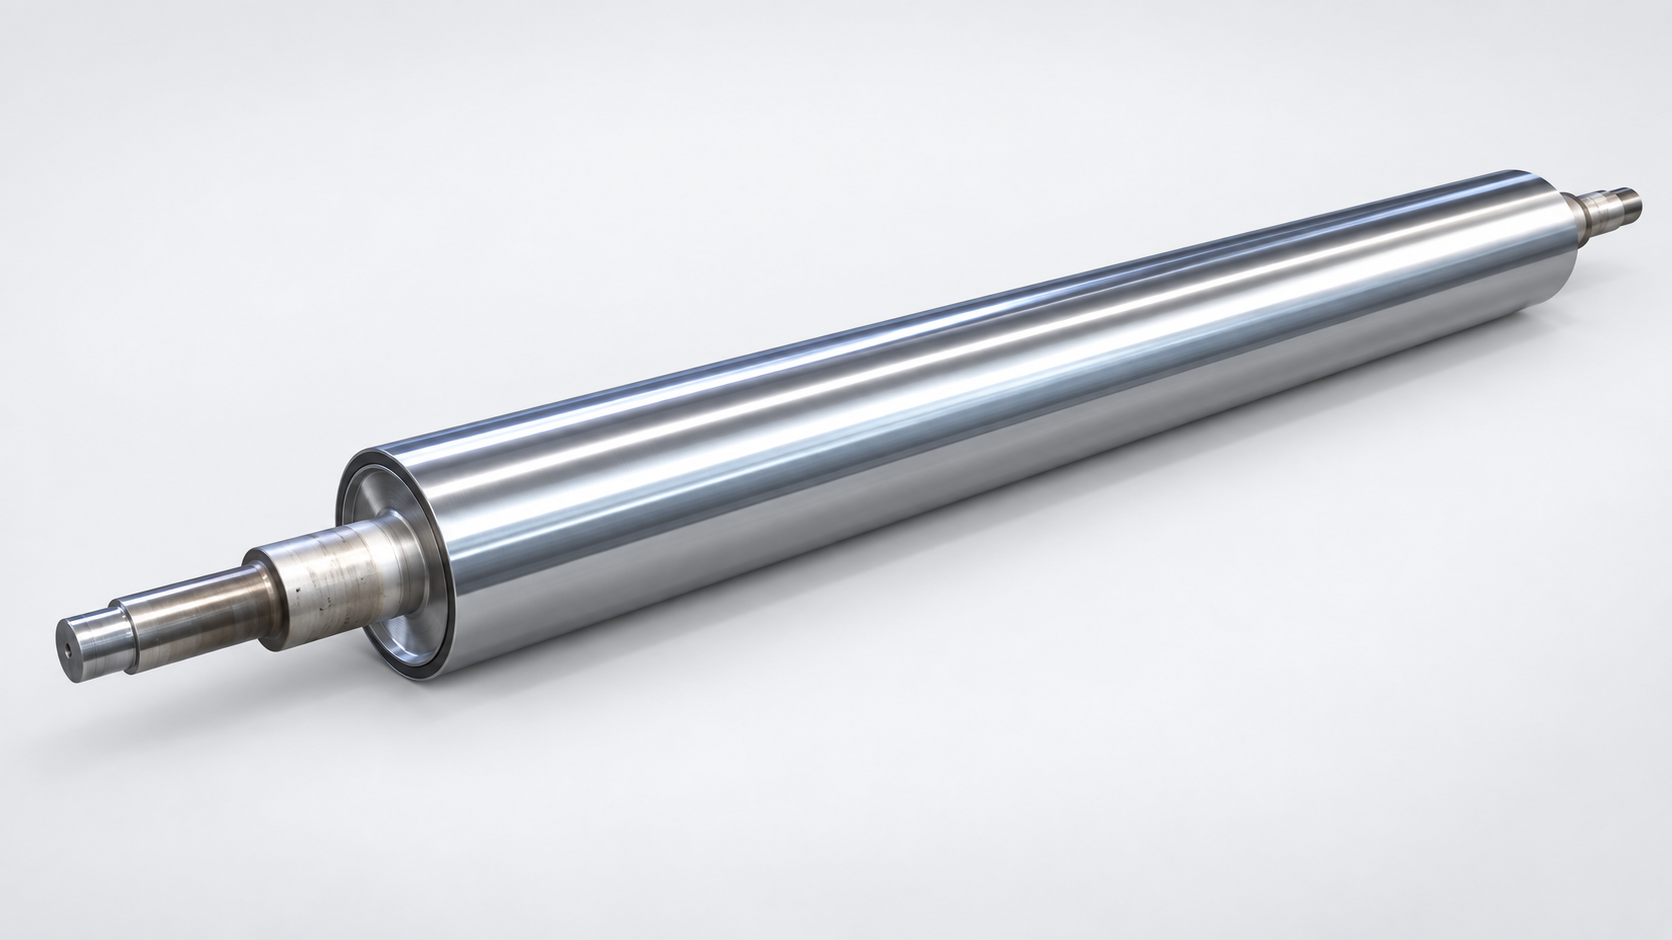
Surface after chrome plating and polishing
After finishing, the chrome coating was 100 µm thick. The measured surface roughness was Ra 0.06–0.18 µm.
PROJECT RESULTS
Final parameters after finishing
| Parameter | Project result |
|---|---|
| Final chrome coating thickness | 100 µm |
| Surface roughness measured after polishing | Ra 0.06–0.18 µm |
| Journals and bearing seats | Good condition; no repair required |
The 100 µm thickness refers to the finished coating after grinding and polishing. The stated Ra range is based on measurements taken after polishing this particular roller.
TECHNICAL ENQUIRY
Enquire about roller reconditioning
Send photos of the damage, the basic roller dimensions and a description of how it operates in the machine. Include details of the existing coating and the required surface parameters, if available.